VMC850 vs VMC855 Vertical Machining Centers: Spec Breakdown for Precision Mold Making
Milling & Machining Center Specialists • 2025-01-28 • 6 min read
Содержание статьи (5)
Choosing Between the Industry Standard VMC850 and the Mold-Optimized VMC855 #
In the vertical machining center category, the "850" footprint is universally recognized as the sweet spot for 3-axis precision milling. However, when evaluating HT Precision's lineup, clients frequently ask: "What makes the VMC855 distinct from the VMC850, and does my application justify the upgrade?"
This engineering guide dissects the architectural differences to help you select the exact configuration for your parts.
1. The Critical 50mm Y-Axis Differential (500mm vs 550mm) #
At first glance, a 50mm increase in travel might seem incremental. In die and mold manufacturing, however, the Y-axis is almost always the limiting geometric bottleneck:
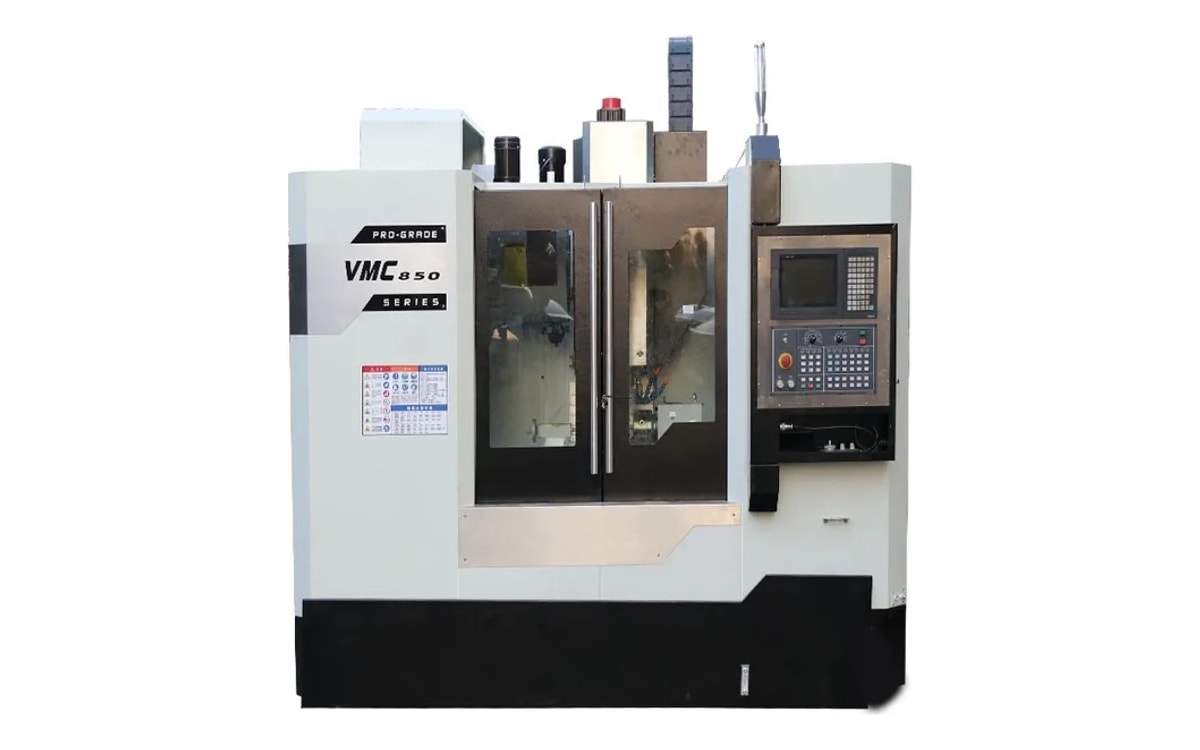
- VMC850 (800 × 500 × 500 mm Travel): Accommodates standard 400mm × 600mm mold bases comfortably. However, when mounting large vice clamps, rotary indexing heads, or extended mold ejection plates, 500mm of Y-travel leaves little safety margin.
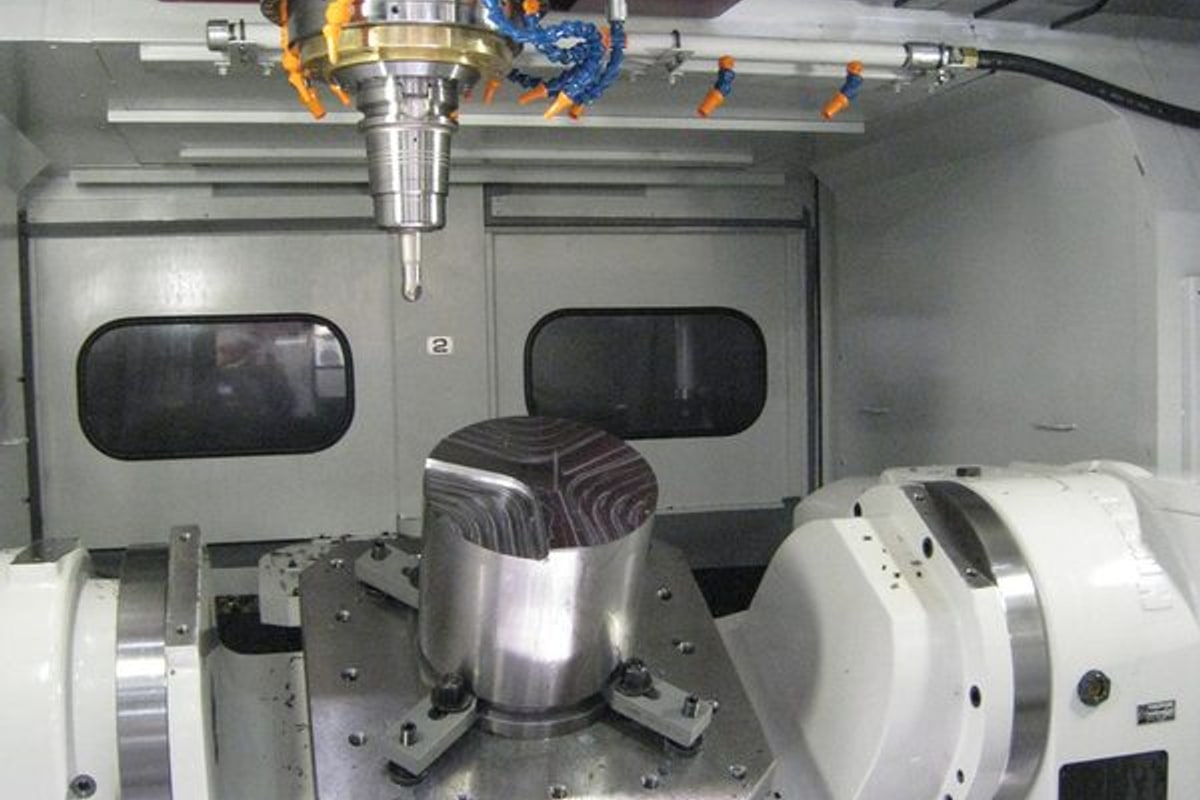
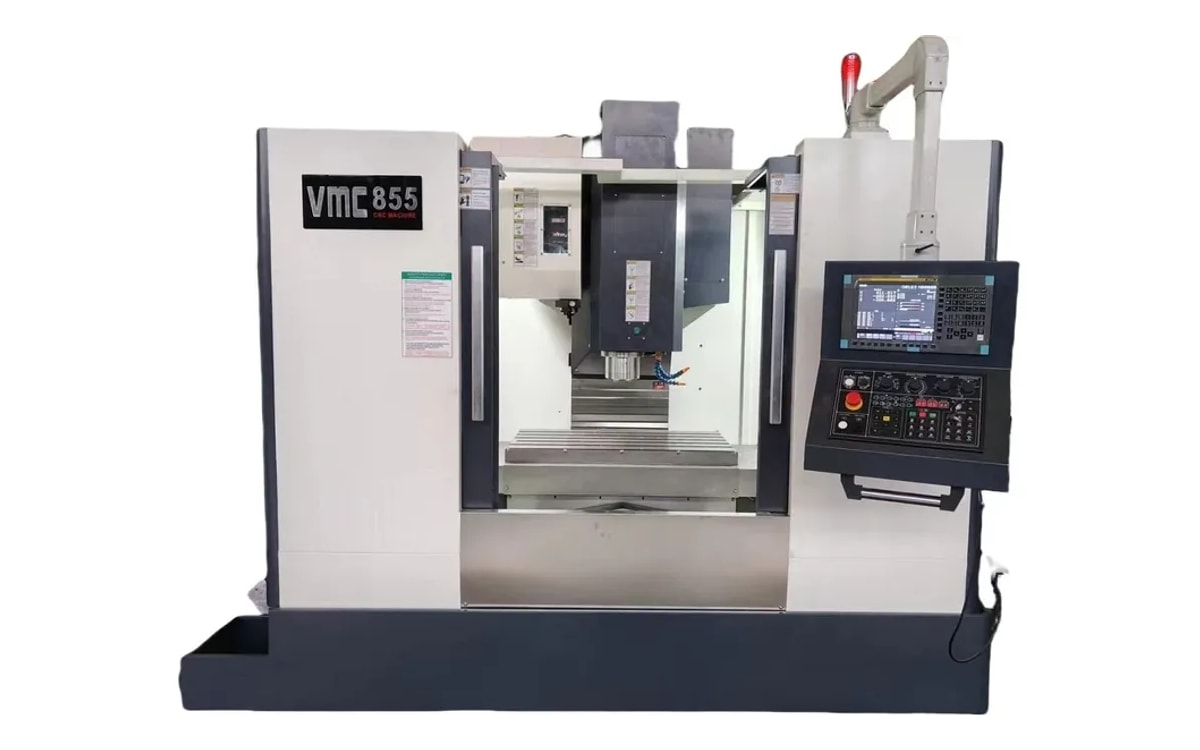
- VMC855 (850 × 550 × 550 mm Travel): The extra 50mm of stroke in both Y and Z directions enables complete pocket milling and perimeter finishing on 500mm mold blocks without repositioning. More importantly, the column throat depth is increased, and the saddle is widened to support the full 550mm stroke without table overhang droop.
2. Guideway Kinematics: Ball Linear Guides vs Heavy Roller Linear Guides #
Rigidity during high-feed milling depends directly on the contact area of the guideway rolling elements:
- Ball Linear Guides (Standard VMC850): Point contact between ball bearings and rail profiles provides low rolling friction, enabling brisk 36 m/min rapid positioning. Excellent for aluminum alloy machining, 3D surface finishing, and light-to-medium steel milling.
- Roller Linear Guides (VMC855 Mold Edition): Cylindrical rollers replace balls, creating line-to-line contact. This increases elastic load capacity and damping stiffness by over 30%, which suppresses high-frequency cutting tool chatter when roughing hardened tool steels like P20, H13, and NAK80.
3. Spindle Thermal Stabilization & Direct Drive #
- VMC850: Standard belt-drive 8,000/10,000 RPM spindle. Well balanced for everyday job-shop versatility and general torque distribution.
- VMC855: Equipped standard with a Refrigerated Spindle Oil Chiller and direct-drive 10,000 / 12,000 / 15,000 RPM inline spindle. By circulating chilled oil through the spindle sleeve jackets, the machine restricts spindle nose thermal elongation to less than 0.005mm even over a 24-hour continuous finishing cycle.
Engineering Decision Flowchart #
- Select the VMC850 if:
- You manufacture automotive brackets, valve bodies, aluminum electronics housings, or general machinery parts.
- Your production emphasis is fast rapid traverse and maximum capital efficiency.
- Select the VMC855 if:
- You specialize in plastic injection molds, die-casting core inserts, or stamping die components.
- You frequently cut pre-hardened steels (HRC 30–48) and require sub-micron mirror surface finishes.
- You plan to mount a heavy 4th-axis rotary table without sacrificing usable Y-axis working envelope.
HT Precision Engineering Team
Specialized in high-rigidity CNC machining centers, slant bed turning solutions, and sub-micron laser pitch calibration protocols.
Станки, упомянутые в статье
 VMC Series
VMC850
Meehanite FC-30High-Rigidity Precision Vertical Machining Center for Mold & Production
 VMC Series
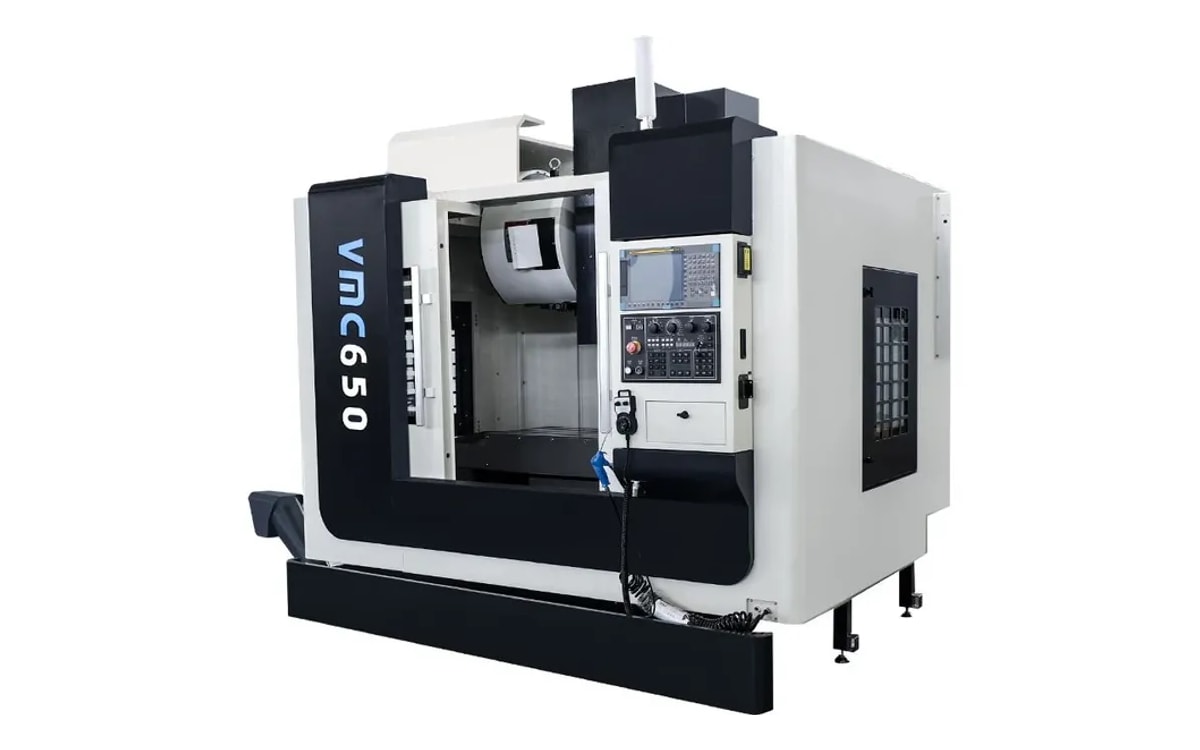
VMC650
Meehanite FC-30Compact High-Speed Vertical Machining Center for Small Parts & Rapid Cycles
 VMC Series
VMC855
Meehanite FC-30Heavy-Duty Precision Mold Machining Center with Extended Y-Axis Travel
Нужна консультация по вашей детали?
Пришлите чертеж детали нашим технологам для расчета машинного времени и подбора инструмента.
Запрос коммерческого предложения
Прямые цены от завода-изготовителя, подбор инструментальной оснастки и компоновочные 3D CAD чертежи за 12 часов.
RFQ Received Successfully
Спасибо! Ваш запрос получен. Наши инженеры подготовят коммерческое предложение и свяжутся с вами в течение 12 часов.
Submission Notice
Ошибка отправки. Пожалуйста, напишите нам напрямую: xiuc32860@gmail.com.